6.51 / .2563 Valve Guide Reamer Engine
| Dc | 6.51 |
|---|---|
| Lt | 145 |
| Lc | 45 |
| flute type | spiral |
| Material | HCS |
| Manufacturer | TOKAR |
| Country of Manufacture | Ukraine |
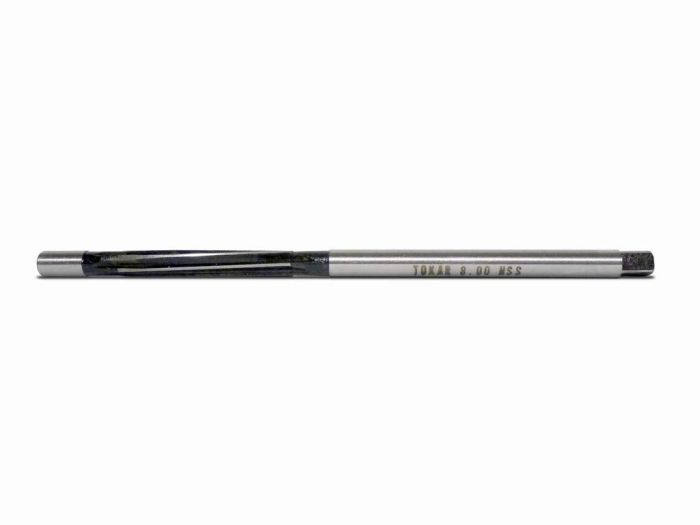


Valve Guide Reamer 6.51 mm (.2563") – Engine Valve Guide Finishing Tool
Valve guide reamer Ø6.51 mm for precision finishing of valve guides in engine cylinder heads.
Used after drilling or rough reaming to achieve final size and surface quality.
Application:
Designed for sizing valve guides in automotive, motorcycle and industrial engines.
Correct guide diameter ensures proper valve stem clearance, stable lubrication and reduced wear.
What it actually does:
Final sizing operation with minimal stock removal.
Because the tool cuts only a light finishing allowance, it improves dimensional accuracy and surface finish without forcing the bore off size.
Diameter 6.51 mm (.2563"):
- Defines final valve-to-guide clearance
- At 6.51 mm, oversize clearance increases stem movement, which can affect oil control and seat contact stability
- No geometry correction — finishing only
Cutting design:
- Spiral flutes improve chip evacuation, which reduces the chance of scoring inside the guide
- Optimized cutting geometry lowers cutting force, which helps the bore remain round through the full guide length
- Stable cutting with low vibration supports a smoother finish
Tool geometry:
The tool geometry is optimized for valve guide finishing operations, providing rigidity and stable cutting performance.
The reamer is equipped with a front guide pilot, which keeps the tool aligned with the existing bore axis during entry and cutting.
This reduces radial runout, limits bellmouthing at the entrance and improves bore consistency.
Material & hardness:
Made from HCS (high carbon steel) with hardness ~HRC 62-64.
Fine carbide structure enables a very sharp cutting edge, so the tool cuts cleanly and produces an improved surface in finishing work.
- High edge sharpness → smooth reaming and low surface roughness
- Low cutting forces → reduced tool deflection and chatter
- Machine finishing → supports fine bore surface quality
- Heat stability: HCS has low hot hardness, so excessive RPM causes rapid edge softening
- Strict speed control required to avoid overheating
- Flood cooling is mandatory because oil removes heat and reduces friction in the guide
- Overheating above ~200°C leads to rapid dulling
- Limit: lower wear resistance compared to HSS
In practice:
Finishing tool only.
Recommended sequence: drilling → rough reaming → finish reaming.
The tool follows existing hole geometry, so final accuracy depends on the previous operation.
Specification:
- Tool type: Valve guide reamer
- Diameter: 6.51 mm (.2563")
- Flute type: Spiral
- Guide type: Front pilot
- Material: HCS
- Hardness: ~HRC 62-64
- Application: Finishing / sizing
- Total Length: 145 mm
- Flute Length: 45 mm
Cutting performance:
- Low material removal
- High dimensional accuracy
- Smooth bore surface
- Requires continuous lubrication
Recommended cutting parameters:
- Cutting speed (Vc): 3–8 m/min
- RPM (Ø6.51 mm): 147–391 rpm
- Feed: 0.03–0.08 mm/rev
- Infeed: single-pass finishing
- Coolant: cutting oil (mandatory)
- Prefer lower RPM because HCS loses edge hardness when heat builds up
- Flood cooling recommended because steady oil flow improves finish and tool life
- Avoid dry cutting because friction can smear guide material
- Do not stop rotation inside the hole because trapped chips can mark the bore
- Ensure proper alignment because the tool follows the existing axis
Use for:
- Valve guide finishing
- Cylinder head repair
- Automotive, motorcycle and industrial engines
Limitations:
- Not for drilling
- Not for heavy stock removal
- Does not correct misalignment
