
13.8 мм Свердло кобальтове Co8% середньої серії по металу DIN 338 RN HSS
| drill bit diameter | 13.8 |
|---|---|
| length total | 160 |
| length cutting | 108 |
| shank type | HA |
| material | HSSCo8% |
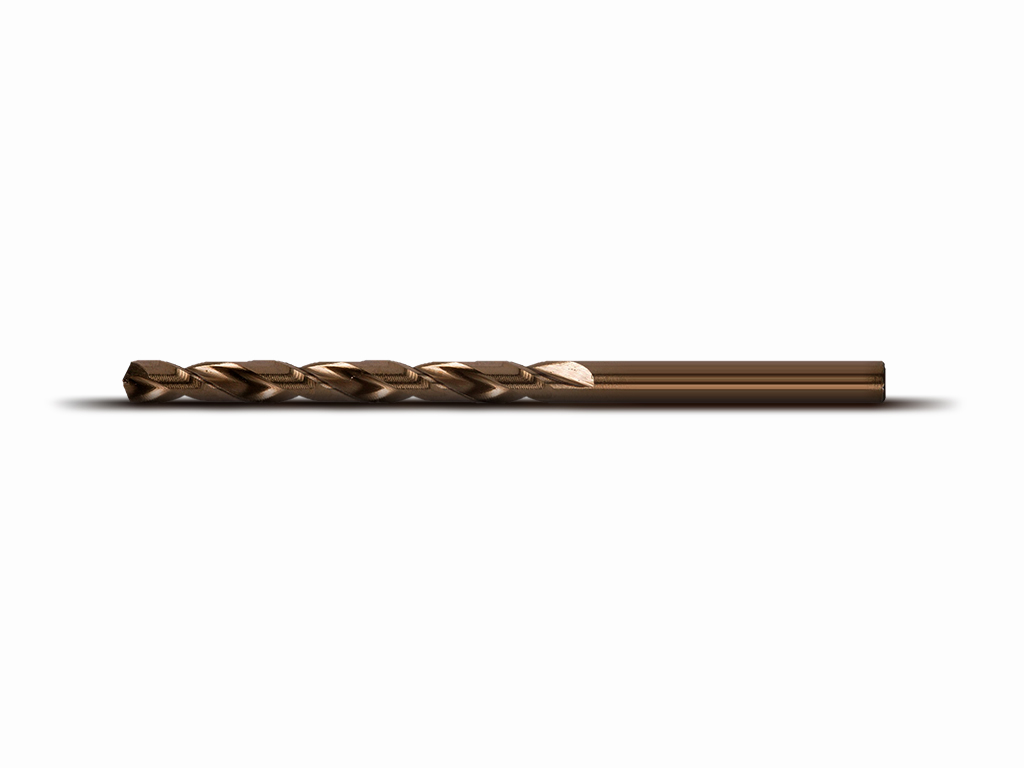
Cobalt Jobber Drills DIN 338 RN HSS Co8%
DIN 338 cobalt jobber drills in RN execution are made from high-speed steel containing 8% cobalt. This alloy provides increased resistance to softening at elevated cutting temperatures. The jobber-length design offers a practical balance between rigidity, drilling depth and reach for metalworking applications.
Applications:
Used for drilling through holes and blind holes in steel, stainless steel and other metals within the manufacturer’s recommended application range. The cobalt-alloyed cutting material is useful where heat at the cutting edge places greater demands on conventional HSS drills.
Operating Principle:
During rotation, the cutting edges remove material while the spiral flutes carry chips away from the hole. The 8% cobalt content helps the cutting material retain hardness at elevated temperatures. Accurate alignment, consistent feed and effective chip evacuation remain essential for reliable drilling.
Diameter and Length:
The drill diameter determines the nominal hole size. Overall length and flute length depend on the selected size. Jobber-length drills provide greater reach than comparable stubby drills, while requiring careful control of tool overhang, runout and lateral loading.
Cutting Material:
HSS Co8% is high-speed steel with 8% cobalt alloyed throughout the material. Cobalt is part of the steel composition rather than a surface coating. Its contribution to hot hardness supports demanding cutting conditions, but suitable lubrication, cooling and cutting parameters are still required.
Tool Geometry:
DIN 338 specifies the dimensional series for jobber-length twist drills. RN identifies the tool execution. Specific point and helix angles, point grinding and surface treatment should be checked in the specifications of the selected drill.
Practical Recommendations:
Clamp the drill securely with the minimum overhang needed and firmly support the workpiece. Apply a steady axial feed and cutting fluid appropriate for the material. When drilling stainless steel, avoid prolonged rubbing without cutting, which can promote work hardening. Monitor chip removal and reduce feed as the drill breaks through.
Specifications:
- Tool type: cobalt twist drill for metal
- Series: jobber length
- Standard: DIN 338
- Execution: RN
- Tool material: HSS Co8%
- Cobalt content: 8%
- Diameter: depends on the selected size
- Overall length: depends on the selected size
- Flute length: depends on the selected size
Cutting Characteristics:
The cobalt-alloyed steel offers increased resistance to heat-related softening compared with conventional HSS. Low runout, stable feed and unobstructed chip evacuation help preserve the cutting edges and maintain hole quality.
Cutting Parameters:
Select spindle speed and feed according to drill diameter, workpiece material and hardness, drilling depth and cooling conditions. Use the manufacturer’s cutting data for the specific drill rather than increasing speed solely because of its cobalt content.
Suitable Operations:
- Drilling through holes and blind holes in metal
- Machining steel and stainless steel within the recommended range
- Preparing holes for tapping or reaming
- Workshop and production drilling requiring increased hot hardness
Limitations:
The 8% cobalt content does not make the drill suitable for every hardened steel or heat-resistant alloy. Avoid bending, impact loads and chip blockage. Drilling depth is limited by tool dimensions and chip evacuation conditions. Holes requiring tight dimensional tolerances may need a subsequent finishing operation.