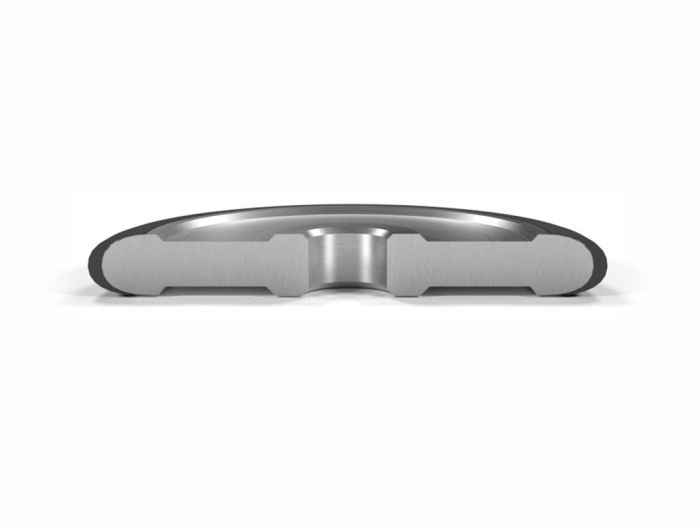
1FF1 flat grinding wheels with double-sided conical profile 100x2x4x4x20 S B2-01 100% AC4 D 91
| D - top diameter | 100 |
|---|---|
| R - radius | 2 |
| X - diamond layer | 4 |
| T - wheel thickness | 4 |
| H - hole diameter | 20 |
| Body | S |
| Concentration | 100% |
| Diamond type | AC4 |
| Size FEPA | D 91 |
| Bond type | B2-01 |
| Type of Operation | Fine |
| Manufacturer | Poltava ZAI |
| Country of Manufacture | Ukraine |


1FF1 Diamond Grinding Wheel – Double-Sided Conical Profile | FEPA D91 (80/63 μm)
1FF1 flat diamond wheel with double-sided conical profile for profile grinding of cutting tool features.
Designed for carbide and other hard brittle materials.
Where it is actually used:
Used for grinding chip-breaking flutes and narrow profiles at the rough stage of profile formation.
Typical applications include:
- Initial shaping of chip breaker geometry on end mills and drills
- Grinding of narrow flutes and grooves
- Profile preparation before transition to micron sequence
The double-sided conical profile enables stable profile generation with controlled contact.
What it actually does:
Productive material removal with basic control of geometry.
Removes bulk material and establishes initial profile shape.
Grain size (D91 ≈ 80/63 μm):
- High stock removal rate
- Typical Ra ~ 0.4–1.0 μm
- Leaves visible grinding marks
Stable and not sensitive to feed or depth.
In practice:
This is a starting wheel for profile grinding.
Used before M63 → M40 → M25 sequence.
Focus is fast geometry formation, not surface quality.
Specification:
- Type: 1FF1 (double-sided conical)
- Abrasive: Synthetic diamond (AC4)
- Grit: FEPA D91 ≈ 80/63 μm (ANSI 170/200)
- Concentration: 100%
-
Body: P / A / S / Ap
(Pressed / Aluminum / Steel / Aluplast)
Body options:
- Pressed: lighter weight, vibration damping, better surface finish
- Aluminum: lightweight with good rigidity, general-purpose solution
- Steel: maximum rigidity for heavy-duty grinding
- Aluplast: balanced weight and rigidity
Why this shape:
- Access to narrow grooves
- Controlled profile generation
- No interference in tight areas
Use for:
- Chip breaker flutes
- Tool profile grinding
- Initial profile shaping
Do not use for:
- Open flat surfaces
- Finishing (use M63 → M10)
- Polishing